Custom Medical Device Packaging
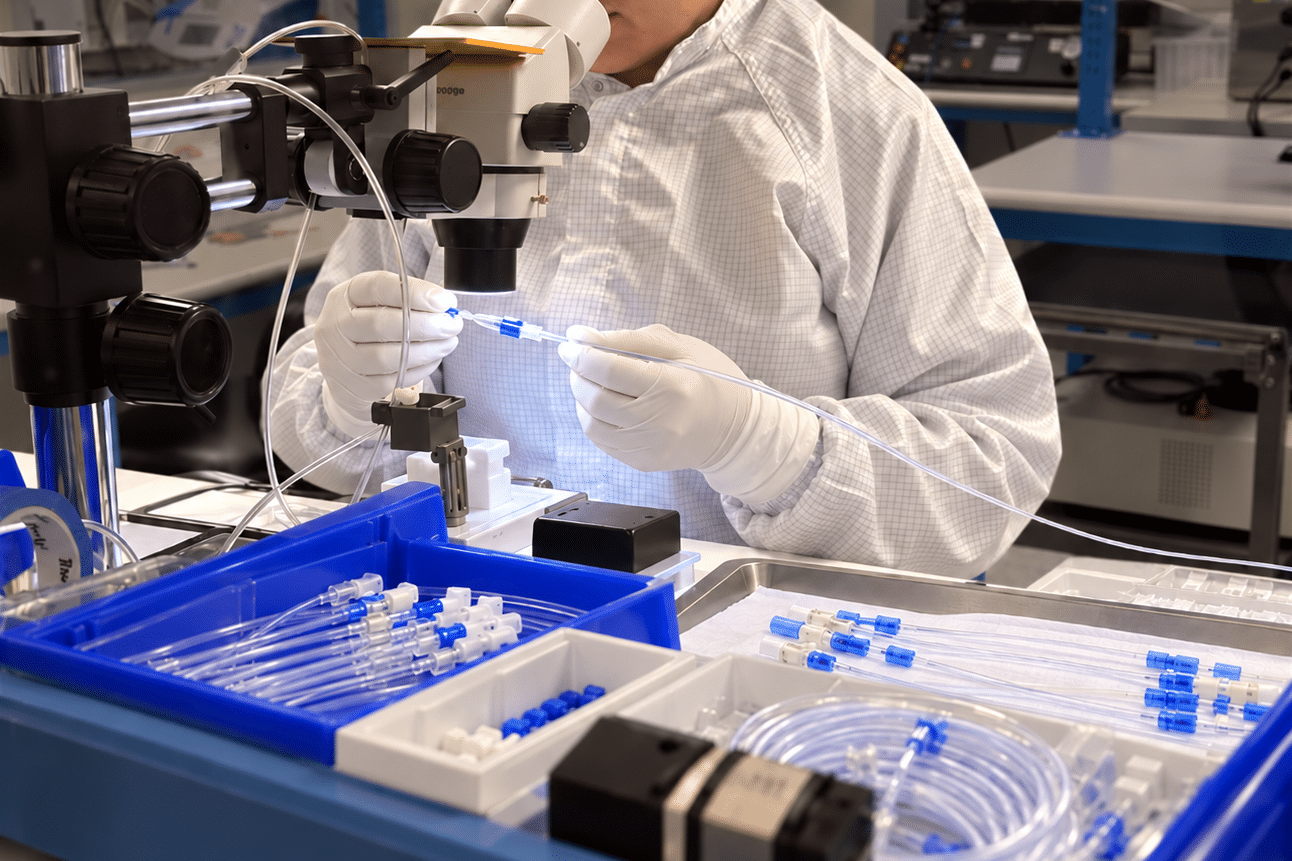
Pathway Medtech provides custom medical device packaging solutions designed to support product protection, sterile barrier requirements, and regulatory compliance. From packaging development and material selection to heat sealing, ISO 11607 validation support, and cleanroom packaging integration, we help medical device companies streamline production and prepare for commercialization.
Custom Medical Device Packaging
Pathway Medtech provides custom medical device packaging solutions designed to support product protection, sterile barrier requirements, and regulatory compliance. From packaging development and material selection to heat sealing, ISO 11607 validation support, and cleanroom packaging integration, we help medical device companies streamline production and prepare for commercialization.


Sterile Barrier Systems for Regulatory Approval
Medical device packaging is not just a protective wrapper. It is a regulated, engineered system critical to device sterility, safety, regulatory compliance, and successful commercialization. A well-designed packaging system protects devices throughout manufacturing, sterilization, distribution, and storage, while supporting FDA, ISO, and EU MDR requirements.
At Pathway MedTech, we provide end-to-end medical device packaging solutions, from early-stage development and prototypes to full commercial production. Our integrated approach ensures packaging is embedded in your overall development strategy, mitigates regulatory risk, and accelerates market readiness.
Why Regulatory-Compliant Packaging Matters
Packaging is a core component of device safety and market success. It must maintain sterility, protect functionality, and meet regulatory expectations. Key objectives of compliant medical device packaging include:
Objective one
Maintaining sterility throughout sterilization, shipping, and storage.
Objective two
Protecting device integrity from handling, vibration, temperature changes, and environmental exposure.
Objective Three
Ensuring devices perform as intended when opened by healthcare professionals.
Objective Four
Meeting labeling and regulatory requirements for UDI, FDA, and EU MDR compliance.
Objective Five
Providing full traceability and documentation for regulatory submissions.
Without a strong packaging strategy, companies risk delayed regulatory approvals, increased FDA inquiries, compromised device performance, and post-market issues. Pathway MedTech ensures packaging is a strategic advantage, not a barrier.

Regulatory Standards and Sterile Barrier System Requirements
Sterile barrier systems (SBS) are highly regulated, and validation is critical to demonstrate device protection and compliance.
Key standards include:
• ISO 11607-1 & 11607-2 – Sterile barrier systems, packaging design, and validation requirements.
• FDA 21 CFR Part 820 / QMSR – Design controls, process validation, and quality management.
• ISO 14971 – Risk management for packaging-related hazards.
• ISTA Standards – Distribution simulation and transportation testing for real-world conditions.
Regulatory agencies expect objective evidence that packaging maintains sterility and device integrity through sterilization, distribution, and storage. Pathway MedTech ensures full compliance through rigorous validation and documentation.
Pathway MedTech Packaging Capabilities
We provide comprehensive medical device packaging services, supporting startups, early-stage programs, and commercial operations.
Sterile Barrier System Development
We engineer packaging to protect devices while ensuring regulatory compliance. Services include:
- Pouch sealing using Tyvek, medical paper, foils, and laminates
- Thermoform tray design and optimized sealing
- Backer card prototyping to protect critical components
- Material compatibility evaluation for EO, gamma, and e-beam sterilization
- Packaging design analysis for device geometry, handling, and risk factors


Packaging Testing and Validation
Pathway performs structured testing to confirm packaging performance under sterilization, shipping, and storage conditions. Services include:
- Seal strength testing (ASTM F88)
- Dye penetration and leak detection (ASTM F1929)
- Burst and pressure testing (ASTM F1140, F2054)
- Accelerated and real-time aging (ASTM F1980)
- Distribution simulation testing (ISTA protocols)
- Post-sterilization performance testing
All results are fully documented for inclusion in Design History Files (DHF), supporting 510(k), PMA, and EU MDR submissions.
Process Validation: IQ, OQ, PQ
Packaging processes must be validated to ensure repeatable, reliable performance. Pathway develops and executes:
- Installation Qualification (IQ) – confirming equipment and setup meet specifications
- Operational Qualification (OQ) – verifying consistent operation across defined ranges
- Performance Qualification (PQ) – demonstrating packaging meets performance requirements under production conditions
- Worst-case seal parameter testing – defining safe operational boundaries
- Process capability studies – quantifying and statistically justifying repeatability
Seal parameters including time, temperature, and pressure are scientifically established to ensure consistent, high-quality packaging across batches.


Labeling and Regulatory Compliance
Proper labeling reduces regulatory risk and ensures device traceability. Pathway supports:
- Unique Device Identifier (UDI) implementation and verification
- FDA 21 CFR Part 801 compliance
- EU MDR labeling standards
- Barcode durability and scannability testing
- Integration of labeling into packaging validation
Integrating Packaging into Design Controls
- Design inputs define sterility, shelf life, and distribution conditions
- Risk analysis per ISO 14971 identifies potential hazards
- Verification and validation protocols confirm performance and compliance
- Full traceability within the DHF supports regulatory submissions
This approach ensures packaging is a validated subsystem, aligned with product safety, regulatory compliance, and commercialization goals.


Supporting Startups and Commercial Programs
Pathway MedTech partners with early-stage startups and commercial programs.
For startups:
- Define packaging requirements for prototypes and verification builds
- Develop testing strategies and validation plans
- Prepare submission-ready documentation for regulatory filings
For commercial programs:
- Optimize existing packaging processes for efficiency and scalability
- Qualify suppliers to ensure consistent materials and production quality
- Implement scalable validation systems for long-term commercial success
Faq
Medical Device Packaging FAQs
Medical device packaging requires careful consideration of material selection, product protection, sterile barrier integrity, and validation requirements. These FAQs address common questions about packaging development, ISO 11607, sterilization coordination, and integrating packaging with medical device manufacturing.
Yes. Pathway MedTech supports medical device packaging development for products moving through development, clinical evaluation, and commercial manufacturing.
Depending on the device, this may include evaluating packaging materials, sterile barrier requirements, product protection, and compatibility with the intended sterilization method. By considering packaging alongside engineering and manufacturing, Pathway helps identify potential design and production challenges before they affect commercialization.
Yes. Pathway can evaluate Tyvek pouch and thermoformed tray packaging solutions based on a medical device’s dimensions, protection requirements, sterilization method, and production needs.
Selecting the appropriate packaging format involves more than material preference. Device geometry, seal integrity, transportation conditions, and product presentation all influence the decision. Pathway helps clients evaluate suitable packaging approaches and coordinate applicable manufacturing and supplier requirements.
ISO 11607 establishes requirements for packaging systems intended to maintain the sterility of terminally sterilized medical devices until the point of use.
The standard addresses sterile barrier system requirements and validation of applicable forming, sealing, and assembly processes. Depending on the packaging design, validation activities may include seal strength, package integrity, distribution testing, and aging studies.
Pathway supports medical device sterilization planning and coordination with qualified external sterilization providers. Sterilization requirements depend on the device, packaging materials, intended use, and selected sterilization method.
Because packaging and sterilization must be compatible, evaluating these requirements together can help prevent material incompatibilities, packaging failures, and avoidable development delays. Pathway works with clients to incorporate applicable sterilization considerations into the broader packaging and manufacturing program.
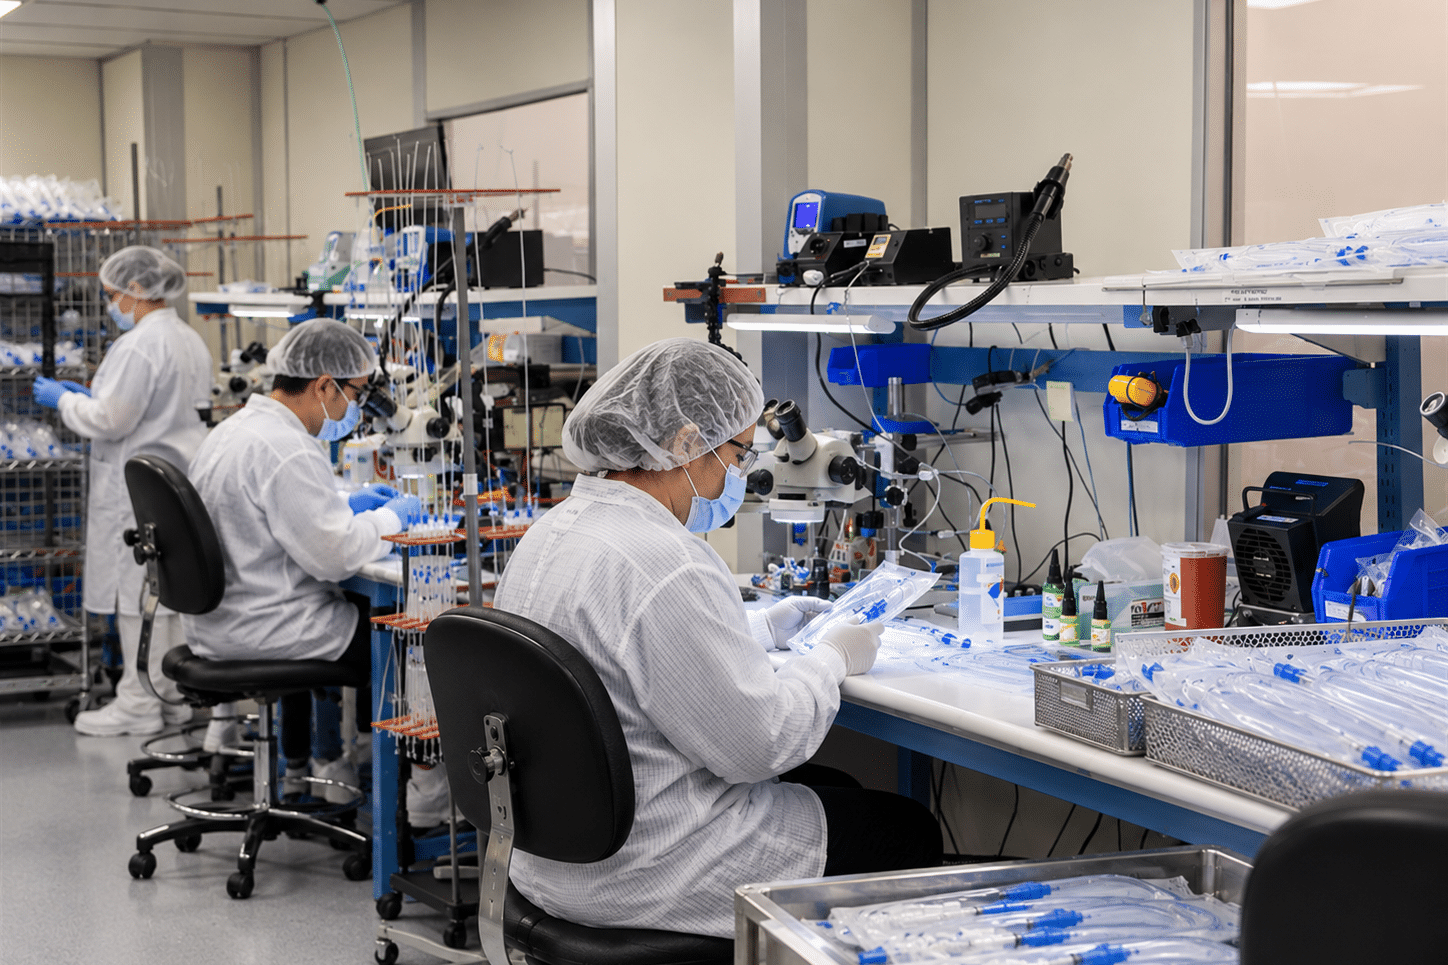
Yes. Medical device packaging can be integrated with ISO Class 7 cleanroom assembly when the device, packaging process, and applicable quality requirements support that approach.
Coordinating assembly and packaging can reduce unnecessary product handling, additional supplier transfers, and manufacturing complexity. Pathway’s cleanroom manufacturing and quality capabilities allow applicable packaging activities to be considered alongside device assembly, inspection, and production documentation.
A medical device packaging project typically begins with the device’s dimensions, intended use, packaging objectives, anticipated production volumes, and any known sterilization or shelf-life requirements.
Existing drawings, packaging concepts, material specifications, and testing information are helpful but are not required for an initial discussion. Pathway begins with a brief introductory call to understand the project. Following a mutual NDA, our team can review confidential technical information and determine the appropriate next steps toward a packaging proposal.
Strengthen Your Medical Device Packaging Strategy
Medical device packaging impacts regulatory approval, device safety, and commercial success. Pathway MedTech delivers comprehensive development, testing, and validation solutions aligned with ISO 11607, FDA requirements, and global regulatory standards. Our hands-on, integrated approach ensures your packaging supports sterilization validation, submission readiness, and successful commercial launch.